Complete Valve Solution for Coal-fired Thermal Power Generation System
September 11, 2026
Full English Article
As the core guarantee of global stable power supply, coal-fired thermal power generation units operate continuously under full and variable load, enduring extreme high-temperature, high-pressure, and steam scouring working conditions. The safety, stability, and efficiency of the entire thermal power system are highly dependent on high-performance, industry-specific industrial valves. As a national high-tech enterprise specialized in the R&D, manufacturing and service of power station valves, Shangtie Valve delivers integrated and customized high-temperature and high-pressure power station valve solutions for full-scenario thermal power systems, covering boiler main steam pipelines, feedwater circulation, flue gas desulfurization and denitrification, and auxiliary piping systems. Our professional valve configurations effectively solve common industrial pain points including thermal deformation, steam erosion, medium backflow, and frequent load switching failure.
Coal-fired power systems impose the most stringent technical requirements on power station valves: 24/7 uninterrupted service, long-term resistance to 540℃ ultra-high temperature and 2500LB ultra-high pressure, anti-cavitation, anti-erosion, bubble-tight zero leakage, and excellent thermal fatigue resistance. Ordinary general-purpose valves are prone to internal leakage, jamming, seal failure and short service life in harsh power plant environments. In contrast, all core valves from Shangtie Valve adopt premium Cr-Mo-V heat-resistant forged steel materials, strictly manufactured in accordance with API, ASME B16.34, DIN, GB and NB power industry standards, fully adapting to the full-cycle extreme operating conditions of coal-fired generating units.
1. Core Valve Failure Pain Points in Coal-fired Thermal Power Systems
A complete coal-fired power generation process includes boiler combustion, steam heat exchange, turbine power generation, flue gas treatment and water circulation, with complex medium components and frequent working condition fluctuations. Conventional industrial valves often face multiple failure risks in power plant scenarios, which directly threaten unit operation safety and increase O&M costs.
High-temperature thermal deformation failure: Long-term exposure to 450℃–540℃ superheated steam causes ordinary cast steel valves to deform, resulting in poor sealing and pipeline medium leakage.
Steam erosion and cavitation damage: High-velocity steam impact and pressure difference cause severe wear on valve internals, reducing flow regulation accuracy and shortening service life.
Medium backflow safety risk: Water pump shutdown or load fluctuation easily triggers medium reverse flow, impacting boiler and pipeline equipment and causing safety accidents.
Fatigue failure from frequent switching: Power grid peak shaving requires frequent valve opening and closing, leading to fatigue damage of ordinary valve structures.
Non-standard matching and high maintenance cost: Mixed use of multi-standard valves leads to poor system compatibility, difficult later maintenance and high replacement costs.
Targeting the above industry pain points, Shangtie Valve relies on 20+ years of power station valve manufacturing experience, a professional R&D team and complete testing systems to launch targeted subsystem valve matching solutions, realizing full-scene safety protection and long-term stable operation for coal-fired power plants.
2. Shangtie Valve Full-system Valve Matching Solution
Combined with the structural characteristics and extreme working parameters of coal-fired thermal power units, Shangtie Valve configures professional customized valves for core power plant systems, covering pipeline isolation, flow regulation, backflow prevention, drainage and pressure stabilization functions. Our product specifications cover DN15–DN1500 caliber and 150LB–2500LB pressure grade, fully meeting all parameter demands of large, medium and small coal-fired power projects.
2.1 Boiler & Main Steam Pipeline System
As the core high-temperature and high-pressure subsystem of thermal power plants, boiler and main steam pipelines bear 540℃ ultra-high temperature and high-speed steam scouring all year round, requiring valves with excellent high-temperature resistance, pressure resistance and anti-erosion sealing performance.
Shangtie Valve Recommended Products:
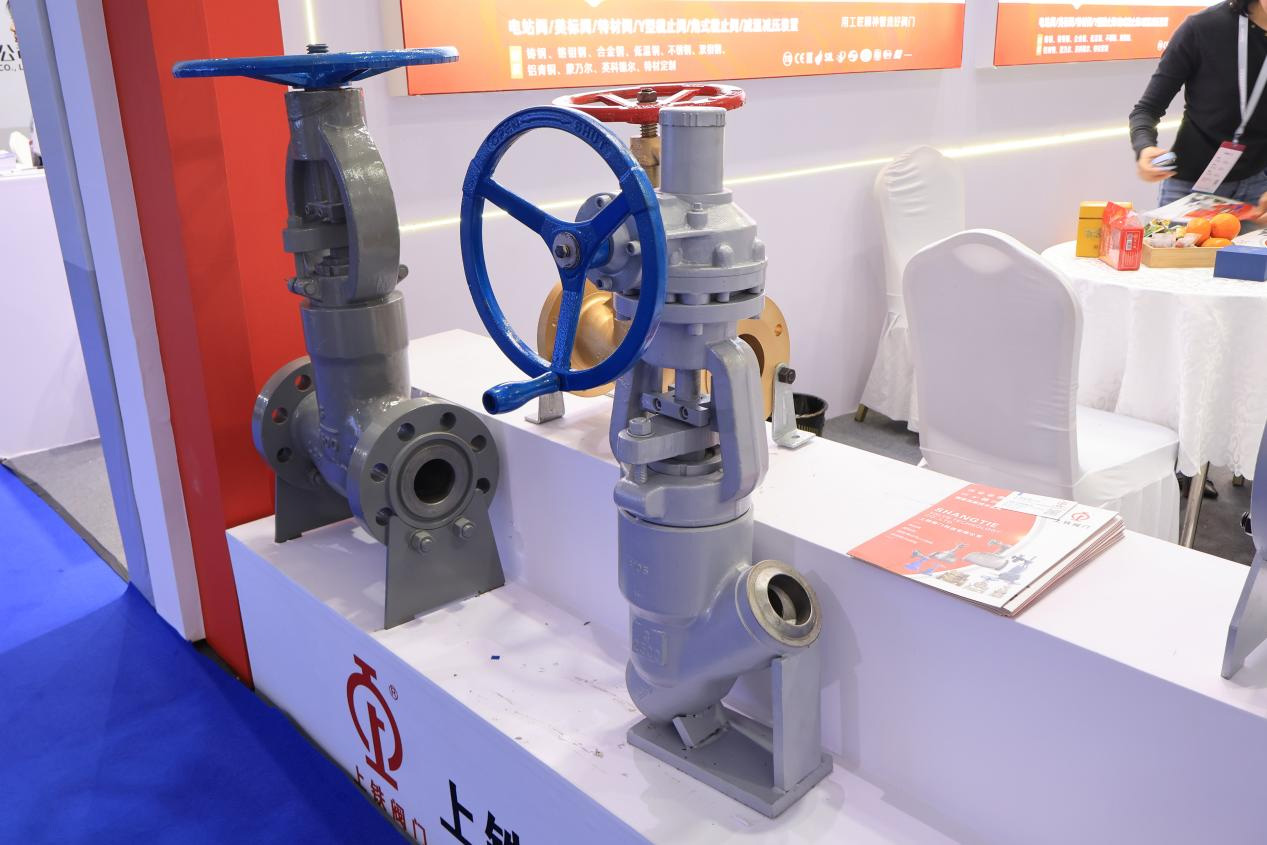
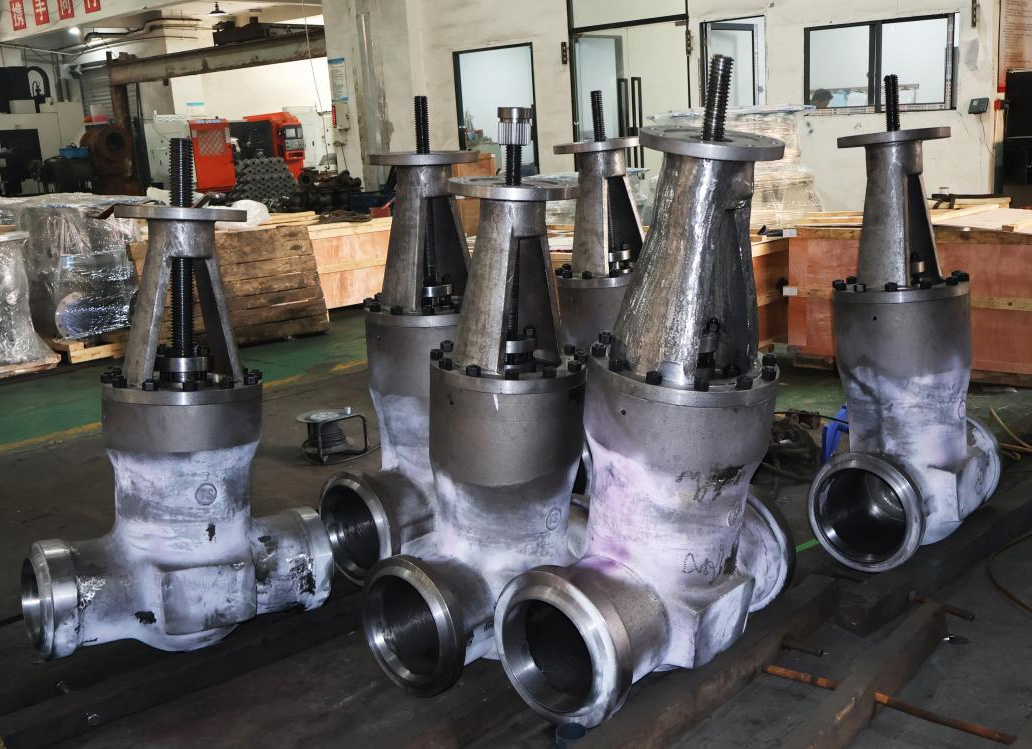
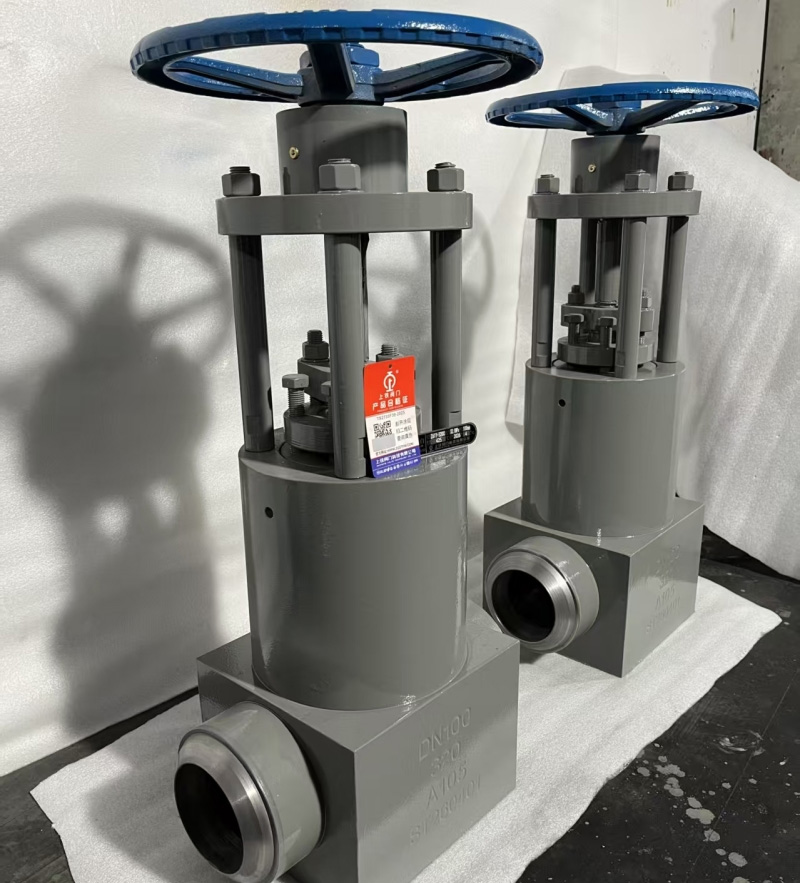
Forged Steel Gate Valves: Adopt full-bore design to minimize flow resistance, equipped with bidirectional metal hard seal structure. Resist high-temperature steam thermal deformation and realize zero-leakage full pipeline cut-off. Compliant with API 6D and API 602 standards, ideal for long-term stable isolation of power station high-pressure steam pipelines.
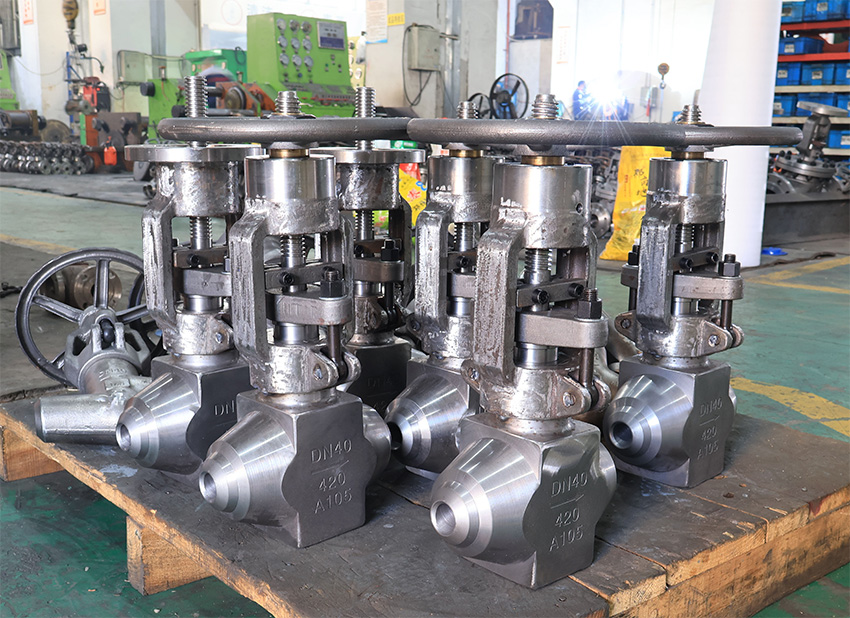
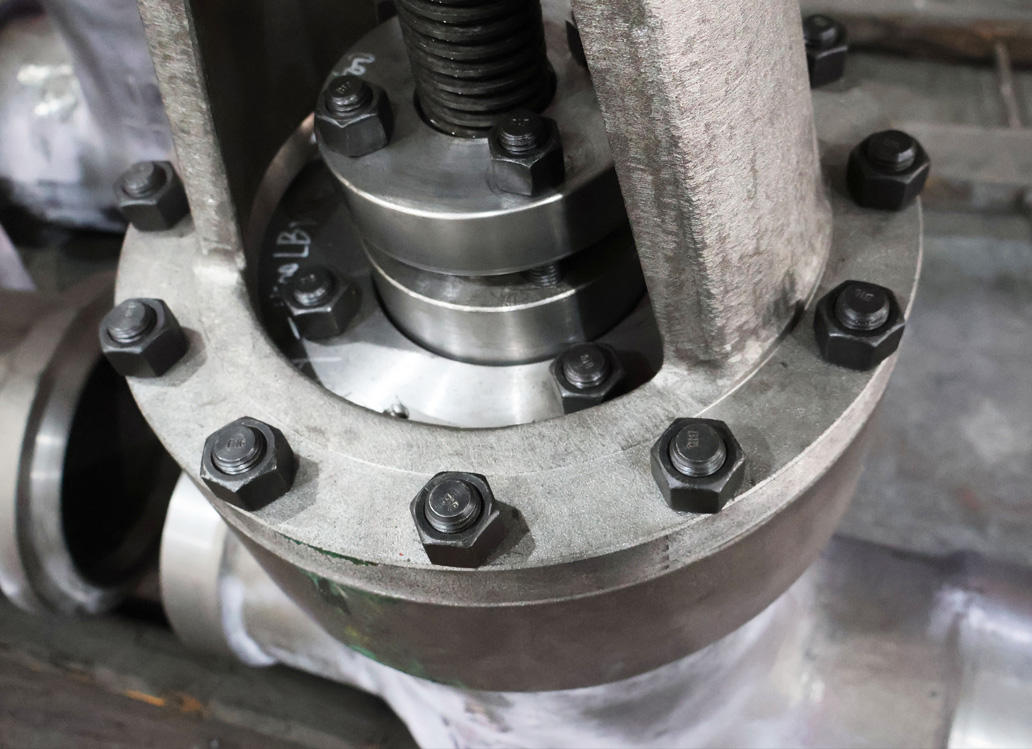
Pressure-sealed Bonnet Globe Valves: Professional power station globe valves with bellows sealing structure, achieving zero fugitive emission. Capable of precise steam flow and pressure regulation, adapting to boiler peak shaving and variable load operation.
High-temperature Drain Valves: Specialized for boiler drainage and exhaust pipelines, effectively remove condensed water in high-temperature pipelines and avoid water hammer impact damage.
2.2 Feedwater & Condensate Recovery System
The feedwater and condensate recovery system undertakes the core water circulation work of thermal power plants, with frequent pressure fluctuations and strict anti-backflow requirements. Valve operational stability directly determines boiler drum water level balance and the safe operation of water supply pumps.
Shangtie Valve Recommended Products:
High-pressure Forged Steel Check Valves: Including swing type and lift type, with integral A105/F304 forged steel structure. Automatically prevent medium backflow during pump shutdown, avoid reverse flow impact on boilers and pump bodies, and protect the safe operation of the entire water supply system.
Precision Throttling Globe Valves: Achieve accurate feedwater flow adjustment, stabilize boiler drum water level, and adapt to unit switching between low-flow start-up and full-load operation.
2.3 Flue Gas Desulfurization & Denitrification System
The flue gas treatment system features corrosive and abrasive mixed mediums, requiring valves with excellent corrosion resistance, wear resistance and stable sealing performance to ensure long-term operation of environmental protection pipelines.
Shangtie Valve Recommended Products:
Industrial Ball Valves & Butterfly Valves: Optimized anti-corrosion sealing structure, resistant to flue gas acid-base corrosion. Suitable for large-diameter flue gas pipeline cut-off and flow regulation, supporting pneumatic and electric actuator automatic control.
2.4 Auxiliary Pressure Regulating & Safety Protection System
Power plant auxiliary pipelines involve multi-stage pressure reduction and pressure relief working conditions. Shangtie Valve customized temperature and pressure reducing devices and supporting valve sets realize step-by-step pressure reduction and stable temperature control, effectively avoiding pipeline pressure surge and vibration damage to ensure system operational safety.
3. Core Advantages of Shangtie Valve Power Plant Valve Solutions
3.1 Full Compliance with International Power Industry Standards
All Shangtie Valve power station valves are manufactured in strict accordance with ASME B16.34, API 6D, API 602, DIN, GB and NB power industry specifications. Our factory has obtained ISO9001 quality system certification, TS special equipment production license, CE, GOST, SIL and other authoritative global certifications, fully meeting the quality and safety standards of domestic and overseas coal-fired power projects.
3.2 Professional High-temperature & High-pressure Material Customization
For core steam pipeline valves, we adopt premium Cr-Mo-V heat-resistant forged steel, which stably withstands 540℃ ultra-high temperature and 2500LB extreme pressure. The specially treated metal hard seal surface effectively resists steam erosion and thermal fatigue deformation, solving the inherent failure problems of ordinary valves in power plant harsh working conditions.
3.3 Full-chain Quality Control & Personalized Customization
We implement full-process quality inspection covering raw material forging detection, precision machining, hydrostatic shell test, seat leakage test and finished product full inspection, ensuring bubble-tight zero leakage for every valve. Meanwhile, Shangtie Valve supports personalized customization of valve caliber, pressure grade, material and driving modes (manual, gear, pneumatic, electric, electro-hydraulic linkage) according to project drawings and actual working conditions.
3.4 Large-scale Production & Global Engineering Service
Equipped with an 18,000㎡ standardized modern workshop and advanced precision processing equipment, Shangtie Valve owns stable large-scale production capacity to support bulk orders for large thermal power projects. With 20+ years of industrial experience, our products are exported to more than 50 countries and regions worldwide, providing one-stop full-cycle services including pre-sales technical solution design, in-production quality supervision and after-sales operation guidance for global power EPC projects.
4. Practical Application Value of Professional Thermal Power Valve Solutions
Adopting customized professional valve solutions for coal-fired thermal power systems can significantly reduce pipeline leakage failure rate, extend valve service life, cut down power plant operation and maintenance costs, and guarantee long-term safe and efficient operation of generating units. For thermal power new construction, renovation and expansion projects, Shangtie Valve’s full-set power station valve supporting solutions realize standardized system matching, greatly improving project construction efficiency and creating sustainable economic benefits for power enterprises.
Conclusion
Coal-fired thermal power generation has extremely harsh working conditions and high technical barriers for supporting valve equipment. Ordinary general-purpose valves cannot meet the long-term stable operation demands of power plants. As a professional and reliable power station valve manufacturer, Shangtie Valve relies on mature R&D technology, strict quality control system and rich power engineering experience to provide complete, stable and cost-effective valve solutions for global coal-fired thermal power projects. Our full-series industrial valves fully cover the whole-scene application demands of boiler steam systems, feedwater circulation systems and flue gas treatment systems.
If you need high-quality high-temperature and high-pressure power station valves and professional pipeline matching solutions for coal-fired thermal power projects, feel free to contact Shangtie Valve for professional technical support and free customized quotation.